T-Drill

T-DRILL PND-54 Power Notcher

A pneumatic notcher and dimpler for branch-tube preparation before brazing. Review its role, tooling and workshop requirements with Logamweld Malaysia.

Back to Portable Solutions ->
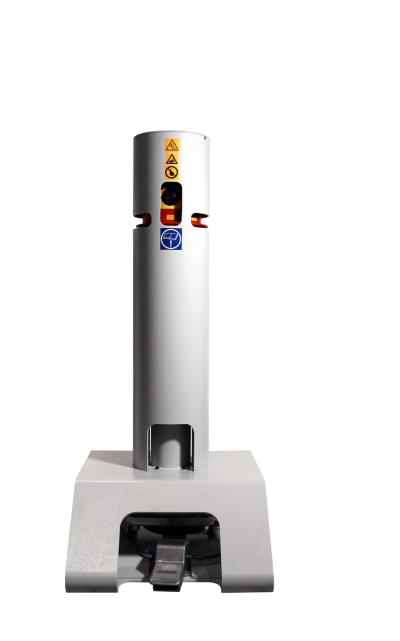
T-DRILL PND-54 Power Notcher
T-DrillPND-54

Product Overview

The T-DRILL PND-54 prepares branch-tube ends for insertion into a formed T-branch collar. It combines notching and dimpling as part of the brazed-joint preparation process.

For Malaysian HVAC, plumbing or manifold fabricators considering this tool, begin with the branch-tube size and joint drawing. The PND-54 prepares the branch end; the collar in the main tube is produced separately. Use the details below to identify the intended operation before requesting the tool and compatible tooling.

Key Specifications

Function
Branch-tube end notching and dimpling
Operating range
12–54 mm; confirm the individual tooling sizes
Power source
Pneumatic
Manufacturer air-supply guidance
600 kPa / 6 bar; confirm the selected configuration
Joint preparation
Branch end for insertion into a T-branch collar before brazing
Positioning features
Depth-stop dimple and second inspection dimple
Where the PND-54 fits in branch-tube preparation

A formed outlet in the main tube and a prepared branch-tube end are separate parts of the joint. The PND-54 addresses the branch end. It is relevant when the specified T-DRILL brazing method requires the notched and dimpled tube to sit correctly in the collar.

For a Malaysian workshop assessing HVAC or plumbing components, send the joint drawing and brazing requirement. This identifies whether branch-end preparation is the step you need to add to an existing manifold process.

What the notches and dimples do

The notcher removes a half-moon-shaped piece from each side of the branch-tube end. At the same time, the tool forms dimples used for insertion depth and inspection. These features have different jobs and should be considered together with the collar and intended joining procedure.

  • The notched profile provides an opening at the inserted branch end.
  • The lower dimple rests on the collar rim as a depth stop.
  • A second dimple, described in the brochure as 6 mm higher, provides an inspection reference.

Confirm tube size, tooling and compressed-air supply

The 12–54 mm operating range covers specified tooling sizes. Confirm the exact branch outside diameter, wall thickness and material instead of assuming every intermediate diameter uses the same setup. The required forming result must also match the joint drawing.

The machine is pneumatically powered. Before selecting a workshop location, check the available compressed-air supply against the manufacturer requirement and confirm the proposed equipment configuration. The official product information provides 600 kPa / 6 bar as guidance.

Prepare a PND-54 enquiry in Malaysia

Send Kumpulan Logamweld the branch-tube dimensions, material and joint drawing, together with the collaring equipment already in use. For copper manifold work, identify whether you are enquiring about the branch-end preparation tool alone or a wider feed-table and collaring arrangement.

Include your Malaysian delivery postcode, required quantity and project timing. The Shah Alam contact route gives you a local place to discuss the requested package and obtain confirmation of availability and any additional support scope.

Questions before you choose PND-54

Does the PND-54 make the outlet in the main tube?

It prepares the branch-tube end by notching and dimpling. The outlet in the main tube is formed with a separate collaring machine. Identify both steps when discussing a complete setup.

Is this the same preparation as trimming a collar for a welded joint?

The PND-54 is described for preparing a branch end before brazing. Collar trimming for a welded connection is a different operation. Confirm the joining method before choosing the equipment.